Industry

Plastic film and extrusion

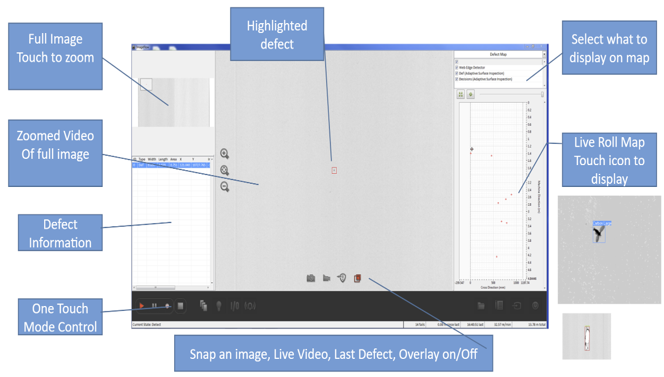
Blown and cast film, medical and window film, battery and polariser film. ImageFlow inspects the full web at line speed on the extruder, Roll Tagger gives every roll an identity and a true position, and Roll Grader grades it against your policy before it ships or goes to the next process.

How One Box fits

Gels, fish eyes and holes mapped to the metre, graded before the roll leaves the line.

ImageFlow on the extruder

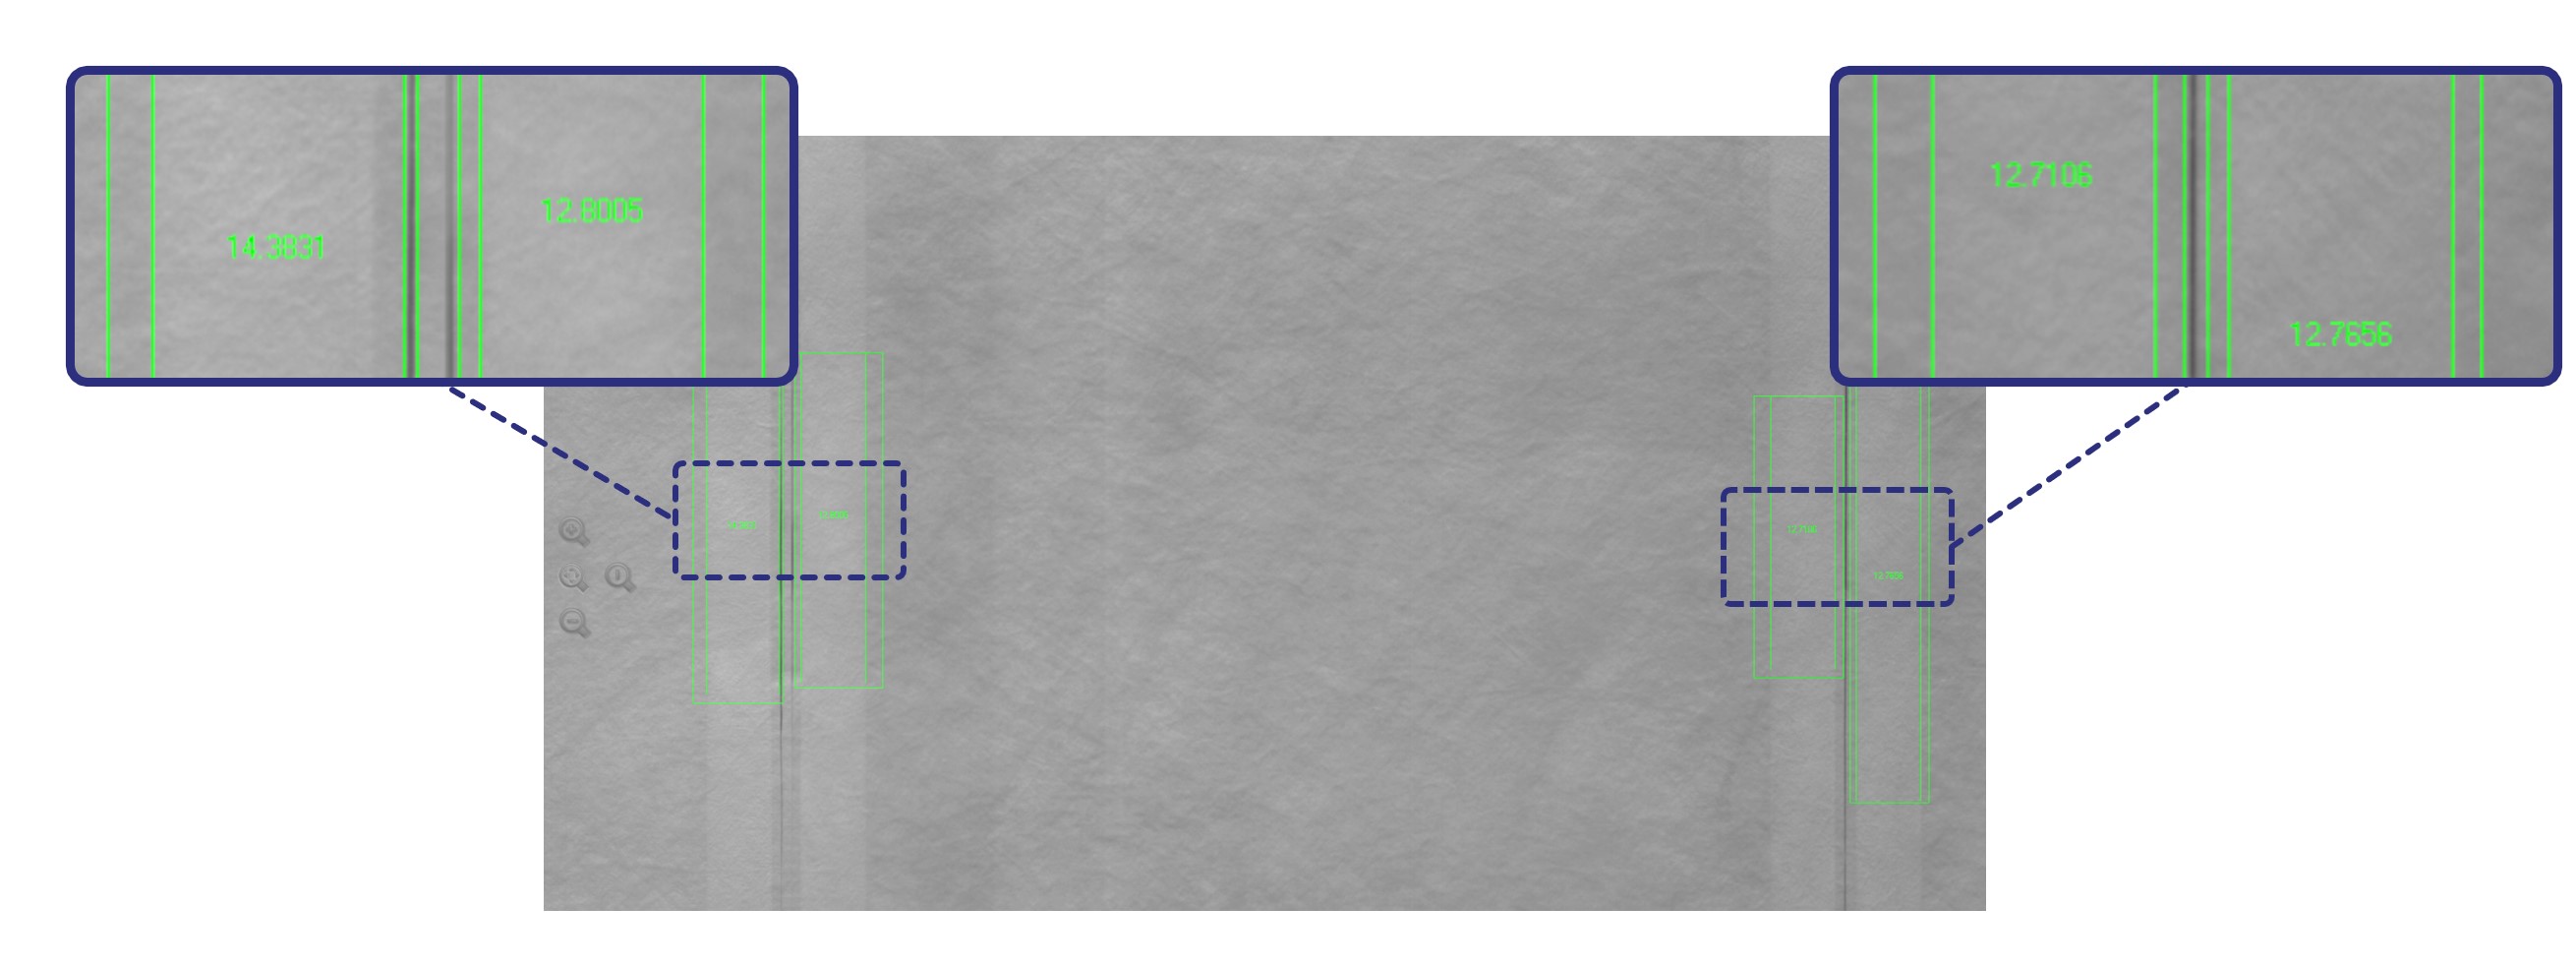
Adaptive surface inspection with the Lotus backlight for clear and translucent film. Block statistics for opacity and density across the web.

Roll Tagger at the winder

Roll identity, encoder truth and operator tags. Every defect is bound to a position on the roll.

Roll Grader as the plant hub

Grade every roll, archive across lines, trace the die line back to the roller that caused it.

What we detect and measure

GelsFish eyesFractured meltsHolesCarbon specksContaminationDie linesWrinklesOpacity and density variationWidth and edge wander

From the line to the daughter roll

Extrude and inspect

ImageFlow detects and classifies every anomaly on the moving web.

Wind and tag

Roll Tagger records the roll, its length and every event at position.

Grade

Roll Grader applies the product's quality policy and plans any rework.

Ship or convert

The graded roll record travels with the roll to the slitter, laminator or customer.

Related solutions

What the patterns tell an extrusion line

Roll Grader reads each defect in the context of the line's state and the pattern it belongs to, and names the likely cause and the first action.

Burst of carbon specks after a screen change

Expected: degraded polymer released from the screen changer. Confirm the decay matches the template; no action unless it persists.

Drifting gel count over a long run

Crosslinked material building in the die or screen, a resin lot with a higher gel count, or die temperature high. Compare with the lot-change event; check die zones; plan a purge.

Streak of die lines at one CD position

Die lip deposit or scratch at that position. Map CD to the die and clean the lip there.

Repeat every N millimetres

The roller with circumference N: nip, chill, embossing, treater or winder lay-on roll. Inspect and clean it.

Step in gels at a roll or lot change

New resin lot or regrind ratio; blend feeder error. Verify lot and blend ratio against the recipe.

Scatter of holes at a stable rate

Contamination in resin or regrind, unmelts tearing in the draw, or moisture. Correlate with regrind ratio and hopper dryer dew point.

Talk to an engineer about your line. Request a demo or read about upgrading an existing inspection system.