Industry

Flexible packaging and converting

Printing, coating, laminating, slitting and bag making. Surface and print inspection on the line, a position-true roll map at the rewind, and automated stop and slow at the slitter and unwind. One roll record from the press to the daughter roll.

How One Box fits

Stop the slitter on the defects that matter and ship a graded roll with a certificate.

ImageFlow on the press or coater

Print inspection and surface inspection in one pipeline, with web-edge tracking and die-cut masking.

Roll Tagger at the slitter and rewinder

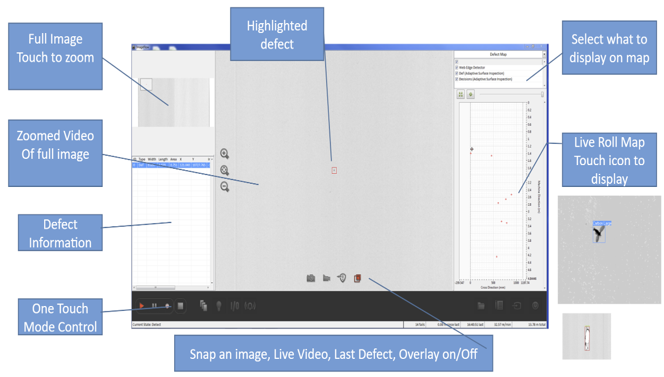
Replays the graded roll map: stop or slow on the defects you chose, let the rest through. No hedgehog of tags.

Roll Grader as the plant hub

Review, grade and plan the slit. Genealogy from master roll to every daughter roll and a certificate per shipment.

What we detect and measure

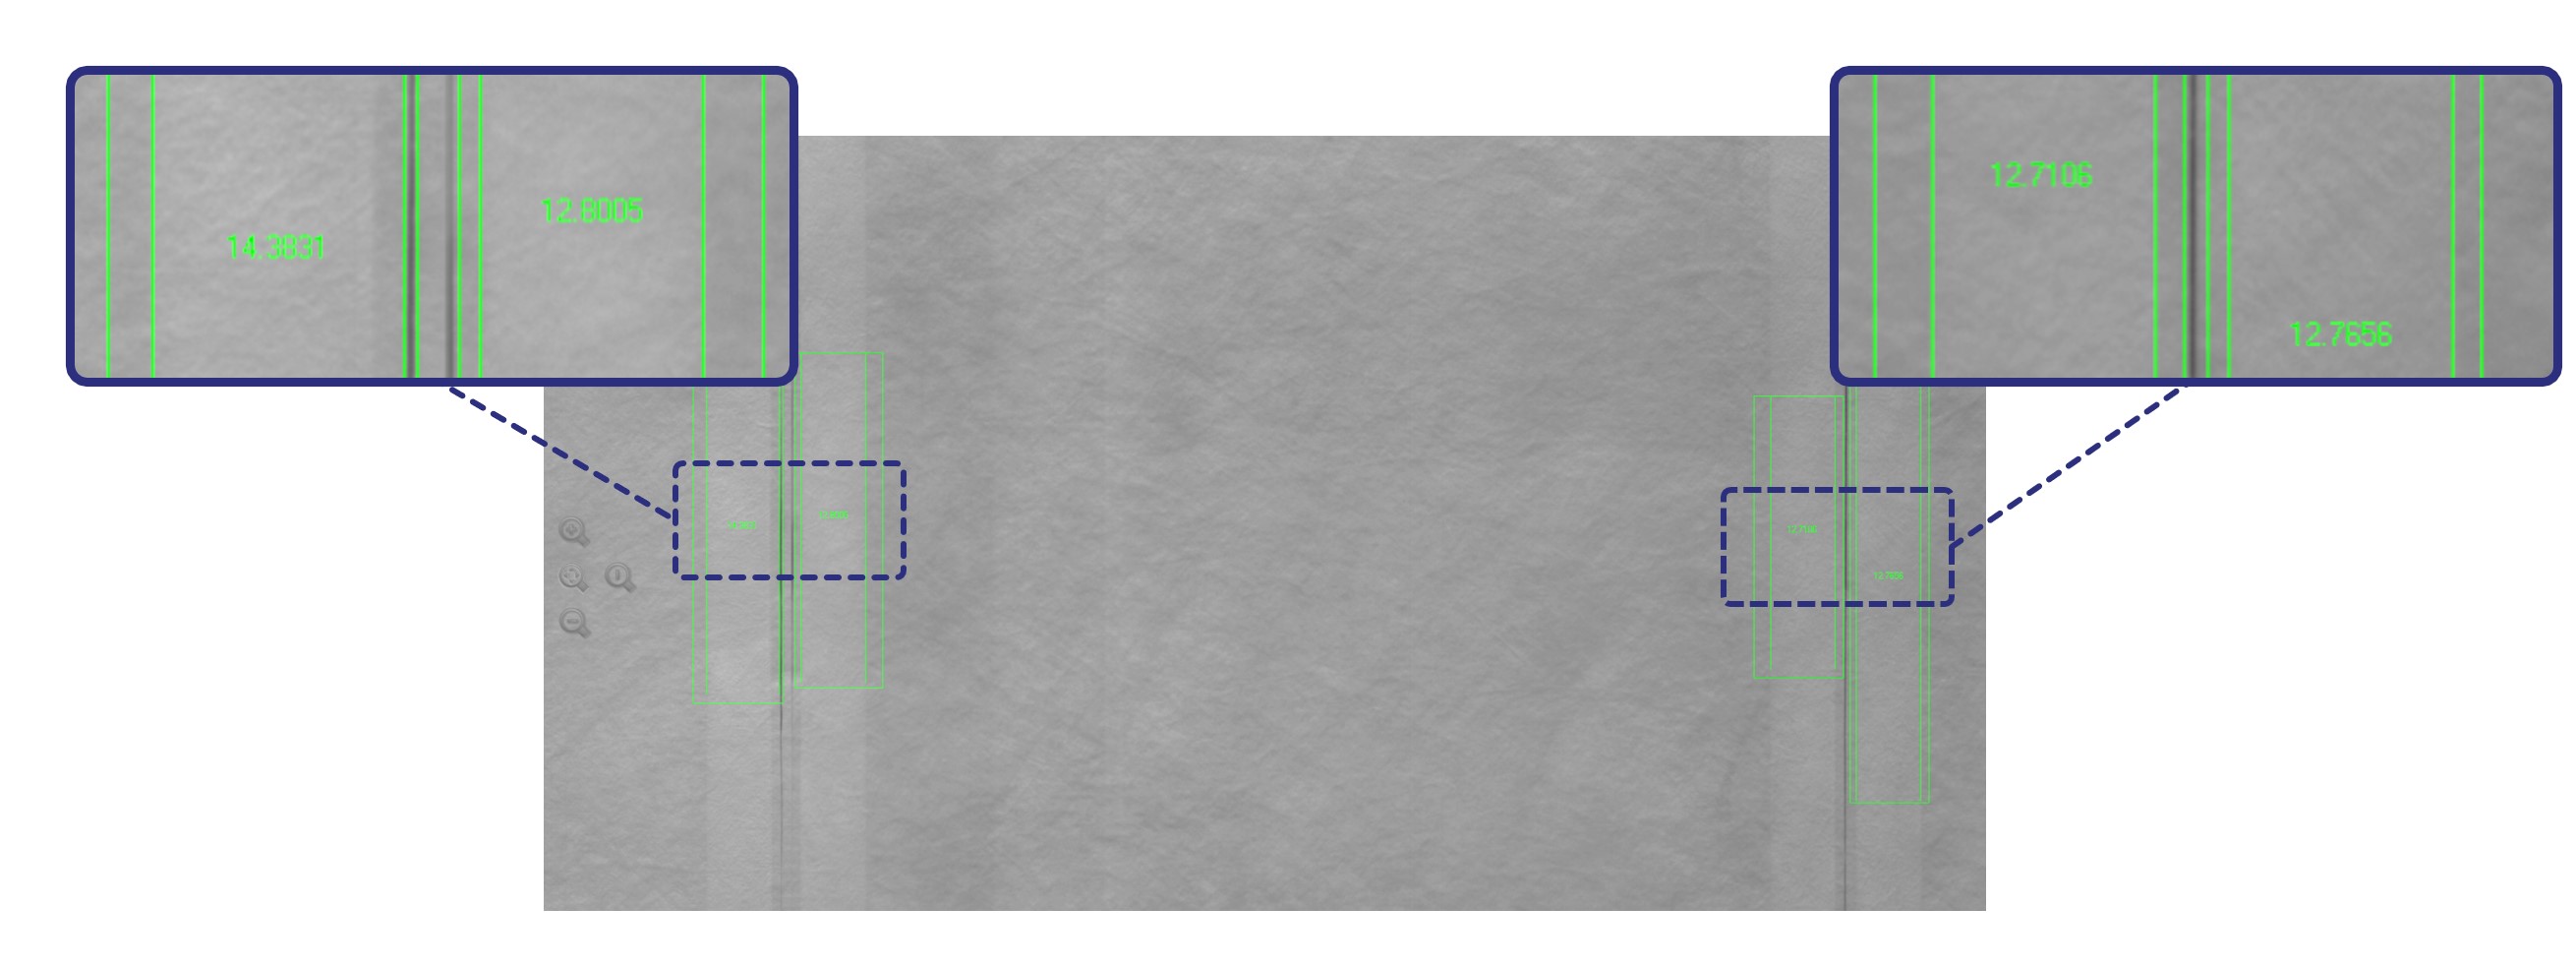
Missing printSmearing, toning and hazingDoctor-blade streaksColour variationRegistration driftCoating voids and skipsSeal defectsHoles and contaminationSplicesCreases and wrinkles

From the line to the daughter roll

Print and coat

ImageFlow inspects every repeat and every square millimetre of surface.

Map at the rewind

Roll Tagger builds the position-true map as the roll winds.

Grade and plan the slit

Roll Grader grades the roll and places the bad metres in scrap, not in the premium order.

Act at the slitter

Roll Tagger stops and slows the slitter on the graded map; daughter rolls inherit their grades.

Related solutions

Every process in the plant, one pattern language

Each web process produces defects with the same handful of shapes on the roll, so the same detectors serve every line; only the cause tables differ.

ProcessWhat inspection looks forWhat usually drives it
Blown and cast film extrusionGels, carbon specks, unmelts, holes, die lines, fisheyes, gauge bands, wrinklesMelt temperature, screen pack age, die temperature, resin lot, purge state
Extrusion coating and laminationPinholes, neck-in edge defects, coat-weight streaks, delamination, contaminationDie temperature, air gap, line speed, primer coverage, chill-roll temperature
Adhesive laminationVoids, tunnels, bubbles, wrinkles, contamination between plies, hazeMix ratio and pot life, coat weight, dryer temperature, nip pressure, tension
Coating (cold seal, heat seal, barrier, lacquer)Skips, streaks, pinholes, coat-weight bands, picking, blockingCylinder wear, doctor blade, viscosity, dryer profile, tension
Gravure and flexo printingMisregister, colour variation, missing dots, hazing, streaks, doctor-blade lines, gear marksCylinder, plate and blade condition, ink viscosity, drying, tension, substrate stretch
Converting (slitting, pouch and bag making)Edge defects, telescoping, seal defects, zipper and spout faults, inherited upstream defectsBlade wear, tension, seal temperature and dwell, roll build

Converting is the first place most inherited defects are caught, so its most valuable rule is "not ours": Roll Grader recognises an upstream line's pattern in the roll genealogy and raises it there.
Talk to an engineer about your line. Request a demo or read about upgrading an existing inspection system.